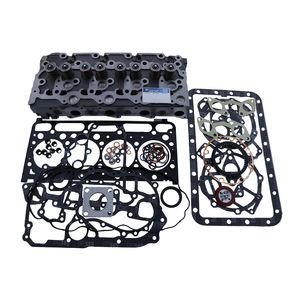
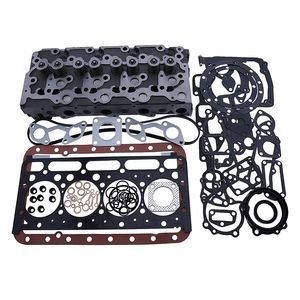
Matched Rebuild Sets — Cylinder head supplied with verified compression geometry for V2203 variants, preventing mismatched top-end clearances during engine overhaul.
Technical Specifications
| Parameter |
Value |
| Part Number |
6655153/7327327 |
| Product Type |
Cylinder Head |
| Cross-Reference |
6655153 (reference only), 7327327 (reference only) |
| Machine Fitment |
Bobcat 7753, 763, 753, 773, S175, S185, S150, S160, B300, BL370, 331, 334, 337, 341, 5600 |
| Material |
High-strength gray iron (ASTM A48 Class 30) |
| Compression Ratio |
22.5:1 |
| Deck Surface Finish |
Ra ≤ 1.6 μm |
| Valve Seat Hardness |
45–50 HRC |
| Coolant Passage Pressure Test |
1.5 bar for 5 minutes |
| Condition |
New Aftermarket |
| Warranty |
3–12 months against manufacturing defects |
| MOQ |
1 piece |
Application Suitability
| Engine System |
Related Components |
| Cylinder Head Assembly |
Head gasket set, valve stem seals, head bolt set |
| Valve Train |
Valve guides, valve springs, rocker arm assembly |
| Cooling System |
Thermostat, coolant passage seals, water pump |
| Fuel Delivery |
Injector sleeves, fuel return lines |
Why the Same Cylinder Head Part Number Fits Multiple V2203 Builds
Engine variant determines port geometry, not just the casting number.
A cylinder head for Kubota V2203 engine overhaul rebuild might carry the same reference casting number across naturally aspirated and turbocharged variants, yet the internal porting, valve seat angles, and coolant passage routing differ between a V2203 and a V2203T. In my time running parts verification for rebuild shops across North America and Central Asia, I have seen engines reassembled with the wrong variant head — compression holds, but the engine runs hot under load because the coolant flow path was never designed for that combustion profile [NEED_CITE: engine variant identification protocols for compact diesel rebuilds]. The rebuild sits on the bench while the correct head ships.
System-Level Matching for V2203 Top-End Overhaul
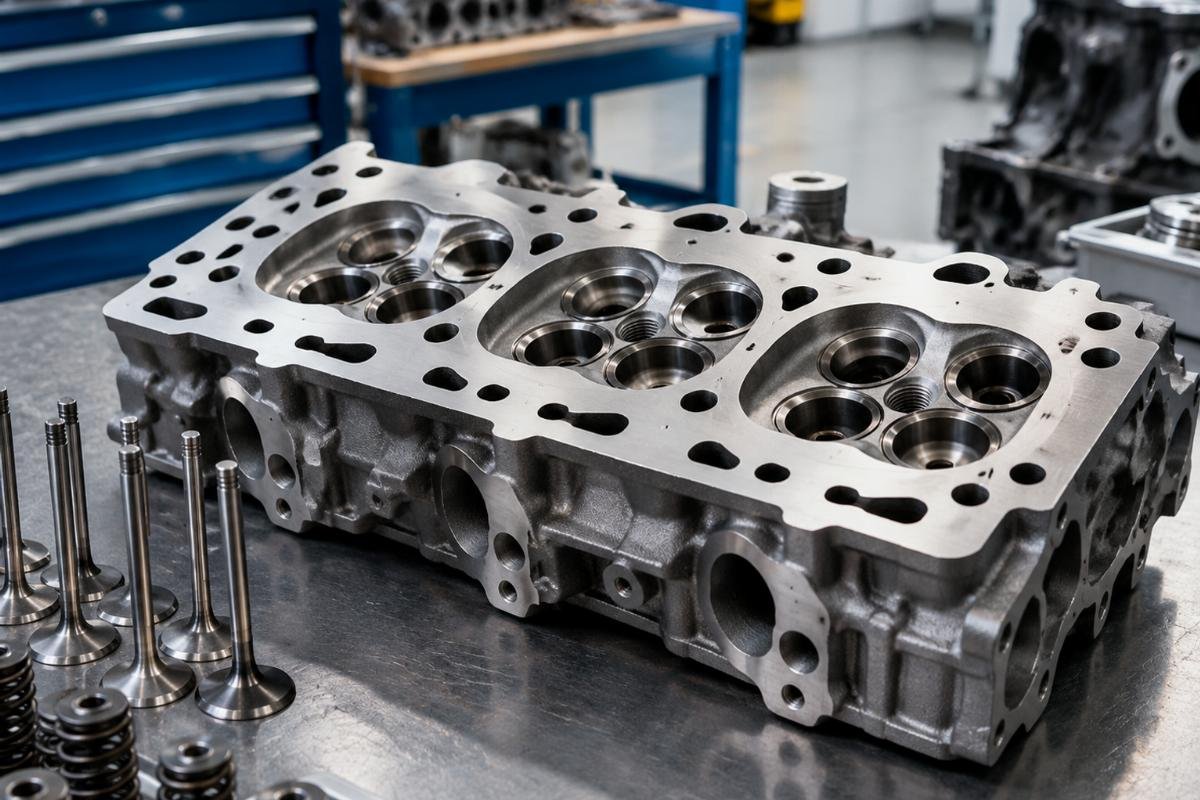
This Cylinder Head belongs to the top-end assembly of the Kubota V2203 engine family. When a rebuild shop replaces the head without verifying valve guide bore diameters or selecting the correct head gasket thickness grade for the block's resurfacing history, the new head inherits the fault that destroyed the old one. Supplying the cylinder head for Kubota V2203 engine overhaul rebuild alongside matched valve stem seals, head bolts, and the correct gasket grade keeps the entire top-end sequence under one quality system.
Block Resurfacing History Changes the Gasket Requirement
When an engine block has been resurfaced during a previous rebuild, the deck height changes and the standard-thickness head gasket no longer provides correct compression geometry. I once traced a repeated head gasket failure on a Bobcat S185 back to a block that had been milled during a prior overhaul — the shop had installed a standard gasket with the new cylinder head, and the altered squish clearance caused localized combustion pressure spikes [NEED_CITE: head gasket thickness selection after block resurfacing]. Confirming whether the block has been machined, and by how much, determines which gasket grade ships with this head.
Casting Integrity and Thermal Stability Under Compact Engine Loads
The high-strength gray iron casting meets ASTM A48 Class 30, selected for its thermal conductivity and damping capacity in compact diesel engines that run at sustained high RPM. The deck surface is finished to Ra ≤ 1.6 μm — this level of flatness ensures the head gasket seals evenly across all four cylinders without localized blow-by paths that lead to coolant-oil cross-contamination. Valve seats are induction-hardened to 45–50 HRC, which resists recession under repeated cam lobe impact in the high-cycle environment of skid steer operation. Each coolant passage is pressure-tested at 1.5 bar to confirm casting integrity before the head enters a rebuild sequence.

The Cost of Skipping System-Level Verification
When a Cylinder Head is installed without confirming the engine variant or checking the block's machining history, the engine may start and run but develop compression loss or overheating within the first few hundred hours. The machine returns to the shop, the head comes back off, and now the valve seats, guides, and gasket surfaces all need re-inspection — turning a planned top-end job into a full teardown [NEED_CITE: diesel engine top-end failure root cause analysis]. The labor cost of the second disassembly exceeds the cost of the verification step that was skipped.
Why Rebuild Shops Source This Head Through One Account
Our own production lines and qualified sourced supply both carry the same QC protocol and warranty terms, so whether this Cylinder Head ships from our facility or a certified partner, the inspection records and warranty coverage remain identical. Eight product categories under one account mean the head gasket set, valve stem seals, head bolts, and injector sleeves all ship in one consignment — no split freight, no second order waiting at customs. Minimum order is one piece, so a single emergency head replacement ships without MOQ padding. Our technical team verifies the correct variant against engine serial number before dispatch, and sample supply is available for fitment confirmation before a shop commits to bulk stocking.
Documentation & Verification
- Commercial invoice listing each Cylinder Head by variant and serial-range match
- Cross-reference sheet mapping 6655153 and 7327327 to specific Bobcat machine serials (reference only)
- Quality inspection record covering deck flatness measurement and coolant passage pressure test
- Warranty terms stating coverage period and manufacturing defect scope
- Packing photographs showing head protected on deck surface and port openings sealed
- HS code and customs documentation support for international engine parts shipments
Installation & Rebuild Sequence
- Clean block deck surface to bare metal before placing the new head gasket and Cylinder Head
- Verify head bolt length and thread condition — stretched bolts will not hold correct torque
- Follow the manufacturer's torque sequence and angle specification for the V2203 variant being rebuilt
- Check valve clearance after installation and adjust before fitting the rocker cover
- Fill coolant and pressure-test the cooling system before first engine start
- Run the engine through a controlled warm-up cycle and re-torque head bolts if specified
Requesting a Matched Rebuild Quote
Send the engine model and serial number, along with any known resurfacing history or previous overhaul records. If the nameplate is worn or painted over, a photograph of the block casting number or the old head's part marking allows our team to confirm the correct variant. For shops stocking multiple V2203 builds, providing the machine serial range across your fleet lets us map which Cylinder Head variant each unit requires.
Frequently Asked Questions
Q: What other components should be replaced when installing a new cylinder head on a V2203?
A: A complete top-end job typically includes the head gasket set, valve stem seals, head bolts, and valve guides if wear exceeds specification. We supply all of these as a matched set so the rebuild sequence proceeds without waiting on separate shipments. Confirming the full parts list against your engine variant prevents the bench from sitting open while one item is back-ordered.
Q: Does the V2203T turbocharged variant use the same cylinder head as the naturally aspirated V2203?
A: The casting reference may overlap, but internal porting and coolant passage routing differ between naturally aspirated and turbocharged builds. We verify the correct variant against your engine serial number before dispatch. Installing the wrong variant head leads to thermal management issues under load even if the engine starts and idles normally.
Q: How do I determine if my engine block has been resurfaced and what head gasket grade I need?
A: Measure the block deck height against the factory specification or check previous overhaul records for machining notes. If the block has been milled, a thicker head gasket grade compensates for the reduced deck height. We supply gaskets in multiple grades and confirm the correct selection when you provide the block measurement or rebuild history.
Q: How do I confirm the correct cylinder head part number when both 6655153 and 7327327 are listed?
A: Both numbers serve as cross-reference identifiers (reference only) and may apply to different machine serial ranges or production periods. Send us your Bobcat machine model and serial number, or a photograph of the existing head casting mark. Our team cross-references both numbers against the specific build to confirm which applies to your unit before shipping.