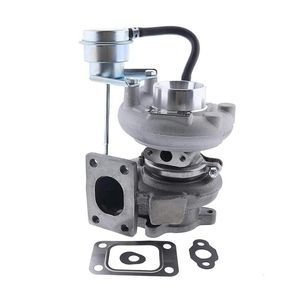
Matched Engine System Supply — Turbocharger 482-8480 shipped with verified gasket sets and oil line seals sized to your C3.8 engine serial variant.
Technical Specifications
| Parameter |
Value |
| Part Number |
482-8480 |
| Cross-Reference |
CA482-8480, 4828480 (reference only) |
| Machine Fitment |
272D2, 272D3, 272D3 XHP, 297D2, 297D2 XHP, 299D2, 299D2 XHP, 299D3, 299D3 XE, 299D3 XHP |
| Product Type |
Turbocharger |
| Engine Compatibility |
Caterpillar C3.8 |
| Condition |
New Aftermarket |
| Turbine Shaft Material |
AISI 8620 forged steel, heat-treated to HRC 58–62 |
| Compressor Wheel Material |
Precision-machined aluminum alloy (A380), dynamically balanced to G1.0 level |
| Turbine Housing Material |
Ni-resist D5S ductile iron |
| Maximum Operating Temperature |
750°C |
| Rotor-to-Housing Clearance |
0.08–0.12 mm |
| Boost Pressure Range |
1.8–2.2 bar |
| Maximum RPM |
120,000 RPM |
| Warranty |
6 months against manufacturing defects |
| Standards |
ISO 9001, ISO 8573-1 Class 4, SAE J1995 |
Application Suitability
| Engine System |
Related Components |
| Intake and forced induction |
Air filter assembly, intake hoses, intercooler passages |
| Lubrication feed and drain |
Oil supply line, drain tube, crankcase breather |
| Exhaust gas routing |
Exhaust manifold gasket, wastegate actuator, clamps |
| Crankcase ventilation |
Piston ring set, cylinder liner condition, blow-by measurement |
Why a New Turbo Fails Before the First Oil Change
A Turbocharger 482-8480 engine rebuild that ignores the root cause of the previous failure means the replacement unit inherits the same destructive conditions. Swapping the turbo without auditing the lubrication circuit, exhaust restriction, or piston ring sealing creates a cycle of repeat failures that drains workshop capacity and erodes fleet availability.
The new turbo is only as durable as the system feeding it. In field teardowns, the majority of premature turbo failures trace back to oil coking from degraded feed lines, compressor wheel erosion from bypassed air filters, or excessive crankcase blow-by forcing oil vapor into the intake tract [NEED_CITE: common root causes of premature turbocharger failure in diesel engines]. I have seen a C3.8 in a quarry application burn through two replacement turbos before the team finally measured blow-by and discovered the piston ring gap had opened past tolerance during a prior overhaul. The turbo was a symptom, not the cause.
System-Level Fault Diagnosis Before Rebuild
Replacing this turbocharger means tracing every path that delivers oil, air, and exhaust gas through the C3.8 platform. The oil feed line runs from the engine block gallery to the center bearing housing, and any restriction or carbon buildup starves the turbine shaft at high RPM. The drain line must flow freely back to the crankcase; a kinked or plugged drain causes oil to back up into the turbine seal and leak past the piston ring seal into the exhaust side. Each of these circuits should be inspected, flushed, or replaced as part of a complete Turbocharger 482-8480 engine rebuild.
Serial Variant Differences Across the C3.8 Platform
The C3.8 engine family spans multiple serial ranges where turbo mounting flange geometry, oil port clocking, and wastegate actuator bracket position shift between production runs. A unit pulled from a 299D2 XHP may share the same base part number as one from a 272D3, yet the oil drain orientation and compressor housing outlet angle differ enough to prevent direct fitment. Confirming the engine serial number before ordering ensures the correct variant ships. Cross-reference verification against superseded part numbers prevents the situation where an older number no longer matches the current turbo casting [NEED_CITE: engine serial variant identification for turbocharger cross-reference].
Material and Clearance Specifications That Matter
The turbine shaft uses AISI 8620 forged steel heat-treated to HRC 58–62, a hardness range that resists journal wear under sustained high-temperature exhaust loading. The compressor wheel is precision-machined A380 aluminum alloy balanced to G1.0 level, which keeps rotor vibration within the threshold that prevents bearing fatigue at speeds up to 120,000 RPM. Rotor-to-housing clearance is held between 0.08 and 0.12 mm; tighter clearance risks contact under thermal expansion, while wider clearance bleeds boost pressure and reduces volumetric efficiency. The Ni-resist D5S ductile iron turbine housing handles sustained 750°C exhaust temperatures without cracking, a material choice driven by the thermal cycling typical in loader applications where engines move between high load and idle repeatedly.

The Cost of Skipping Root-Cause Verification
Installing a fresh turbo on an engine where oil contamination or blow-by remains unaddressed produces a predictable sequence: the new unit's bearing surfaces score within the first several hundred hours, the turbine seal begins leaking oil into the exhaust, and the machine returns to the workshop with the same symptoms that prompted the original repair. This pattern compounds when rebuild shops treat each component as isolated rather than evaluating the intake, lubrication, and exhaust circuits as a connected system [NEED_CITE: diesel engine rebuild best practices for turbocharger longevity]. The labor cost of pulling a failed turbo a second time, combined with machine downtime and a second replacement unit, far exceeds the time required to pressure-test oil lines and measure crankcase blow-by during the initial teardown.
Procurement Backed by System Knowledge
Our own production lines and qualified sourced supply carry the same QC and warranty terms under one account, so a turbocharger and its matching gasket set ship with unified documentation. Eight product categories mean the intake hoses, oil drain gaskets, and exhaust manifold studs your C3.8 rebuild requires can consolidate into a single consignment rather than arriving on mismatched schedules. Orders start from one piece, so an emergency single-unit replacement is never blocked by minimum quantities. Identification is possible from a part number, machine model, photograph, or nameplate image, which matters when the turbo data plate is heat-scaled beyond readability. Cross-reference verification covers superseded and alternate numbers to prevent variant mismatches. A technical team is available to confirm compatibility, grade, and serial-range suitability before you commit to bulk quantities [NEED_CITE: aftermarket turbocharger quality inspection and balance test standards].
Documentation & Verification
- Commercial invoice and packing list itemizing turbocharger and matched gasket sets
- Part compatibility sheet noting engine serial range and cross-reference only designations
- Quality inspection record covering dynamic balance, rotor clearance, and boost pressure test
- Warranty terms document specifying six-month coverage against manufacturing defects
- Packing photographs showing anti-rust oil application, foam cushioning, and carton reinforcement
- HS code and customs documentation support for international engine parts shipments
Installation & Rebuild Sequence
- Pre-lube the center bearing housing with clean engine oil before initial cranking to prevent dry-start scoring
- Verify oil feed and drain line internal diameter matches C3.8 flow requirements for this turbocharger variant
- Torque turbine housing and compressor housing fasteners to C3.8 service manual specifications in sequence
- Confirm rotor-to-housing clearance remains within 0.08–0.12 mm after all mounting hardware is secured
- Run the engine at idle for initial minutes to verify oil return flow before applying load
- Measure boost pressure at rated RPM to confirm delivery falls within the 1.8–2.2 bar operating range
Request a System-Matched Quotation
Provide your C3.8 engine serial number, machine model, and any known rebuild history so we can confirm the correct turbocharger variant and matching gasket grade. If the previous failure included oil consumption or blow-by symptoms, note those details so we can recommend adjacent components to inspect or replace alongside the turbo. We supply complete overhaul kits that include matched piston ring sets, bearing shells, and seal kits sized to your engine's current bore condition.
Frequently Asked Questions
Q: What other components should I inspect or replace when installing a new Turbocharger 482-8480?
A: Inspect oil feed and drain lines for internal carbon buildup, verify the air filter housing and intake hoses are airtight, and measure crankcase blow-by to rule out excessive piston ring wear. Replace the exhaust manifold gasket and turbo mounting hardware. Any degraded oil line should be swapped rather than flushed, as internal flaking will reach the new bearing surfaces within hours.
Q: How do I confirm the correct turbo variant for my specific C3.8 engine serial?
A: Provide the full engine serial number from the block data plate. The C3.8 platform has oil port clocking and wastegate bracket variations across serial ranges. We cross-reference your serial against fitment records to verify flange orientation, drain position, and compressor outlet angle match your engine build before shipping.
Q: What causes premature turbo failure on C3.8 engines in loader applications?
A: The most frequent causes are oil starvation from coked feed lines, compressor wheel erosion from bypassed air filtration, and oil contamination from excessive blow-by pushing past worn piston rings. Loaders cycle between high load and idle frequently, creating thermal stress that accelerates oil degradation in poorly maintained lubrication circuits.
Q: Do you supply complete overhaul kits that include the turbocharger?
A: Yes. We consolidate turbocharger, gasket sets, piston ring sets, main and rod bearing shells, and seal kits into a single shipment matched to your engine serial and current bore size. Each component carries the same warranty terms, and the complete kit ships under one commercial invoice with full cross-reference documentation.
Q: How do I verify boost pressure after installing the Turbocharger 482-8480?
A: Connect a calibrated boost gauge to the intake manifold test port and run the engine at rated RPM under load. The target range is 1.8–2.2 bar. Readings below this range suggest an intake leak, exhaust restriction, or wastegate actuator fault. Readings above the range may indicate a stuck wastegate that risks over-boosting and engine damage.