Block & Internal Parts
Crankshaft 1G871-23012 Replacement for Kubota V1505 Powertrain
<p>Overhaul kit contents verified item-by-item against your specific V1505 build before dispatch</p>
View Details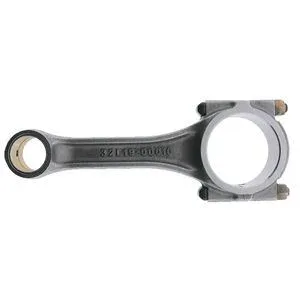
<p><strong>Connecting Rod 103-9680 (cross-reference only) — Engine Grade, high-strength forged steel</strong> for CAT 3044C, C3.4 and 3046 engine rebuilds.</p> <ul> <li>Part of the block and internal rotating assembly — must be matched with correct con rod bearings, piston assemblies, and fasteners to ensure balanced cylinder loading.</li> <li>Confirm oversize or undersize grade required based on crankshaft journal measurement history before ordering.</li> </ul> <p>Dimensional grade matched to your engine rebuild record, supplied as a verified set.</p>
MOQ
1 Piece
Lead Time
2-5 Business Days
Shipping
120+ Countries
Warranty
3-12 Months
Compatible Brands
Engine Grade Matched — Connecting rod assemblies verified against crankshaft journal history and prior rebuild records before dispatch.
| Parameter | Value |
|---|---|
| Part Number | 103-9680 |
| Product Type | Connecting Rod |
| Cross-Reference | 1039680, CA1039680 (reference only) |
| Machine Fitment | 236B, 236B3, 242B3, 246C, 252B, 252B3, 256C, 262C, 262C2, 268B, 272C, 277C, 277C2, 279C, 279C2, 287C, 287C2, 289C, 289C2, 297C, 299C, 315, 315B, 315C, 317B LN, 318B, 906, 906H, 907H, 908H, 257B3, 267B, 277B, 287B, 933, 933C, 939, 939C, D3C III, D3G, D4C III, D4G, D5C III, D5G |
| Engine Fitment | CAT C3.4, CAT 3044C, CAT 3046 |
| Material | High-strength forged steel |
| Tensile Strength | ≥1,200 MPa |
| Hardness | HRC 32–36 |
| Center-to-center Length Tolerance | ±0.05 mm |
| Big-end Bearing Surface Finish | Ra ≤0.4 μm |
| Inspection Method | Magnetic particle inspection (MPI) |
| Condition | New aftermarket |
| Warranty | 6-month warranty against manufacturing defects |
| Minimum Order Quantity | 1 piece |
| Quality Standards | ISO 9001, SAE J470, ISO 683-4 |
| Engine System | Related Components |
|---|---|
| Block & Internal Rotating Assembly | Matched con rod bearings (STD / undersize), piston assemblies, wrist pins |
| Lubrication Circuit | Oil pump, oil cooler, gallery plugs, pressure relief valve |
| Fastener & Torque System | New rod bolts, torque-to-yield fasteners, cap alignment sleeves |
| Overhaul Gasket Set | Head gasket, sump gasket, crankcase seals, rod bolt seals |
A replacement connecting rod installed without verifying the crankshaft journal grind history almost guarantees a repeat teardown within weeks.
Workshops frequently pull engines with spun bearings only to find the previous rebuild used standard-size shells on a crankshaft ground to 0.25 mm undersize. The connecting rod itself was dimensionally correct, but the bearing clearance collapsed under thermal load. In other cases, the big-end bore was honed during a prior repair, shifting the rod into a different weight class and creating destructive imbalance at operating RPM. These are not manufacturing defects — they are identification failures that compound with each rebuild cycle [NEED_CITE: engine rebuild clearance verification procedures for medium-duty diesel engines].
The Connecting Rod 103-9680 (cross-reference only) occupies the critical junction between reciprocating mass and rotational output in CAT 3044C, C3.4, and 3046 engines. It transfers combustion loading from the piston through the wrist pin into the crankshaft journal, meaning any dimensional deviation or weight mismatch propagates directly into bearing wear and vibration. An engine rebuild kit that treats this component as interchangeable across all serial variants ignores the fact that CAT production runs introduced changes in rod bolt specification, big-end bore diameter, and piston-to-rod pairing requirements over the life of these engine platforms. Procurement must therefore begin with the engine serial number and prior overhaul documentation rather than the base part number alone.
Every time a crankshaft is reground, the connecting rod bearing shells must shift to the corresponding undersize grade. A workshop that does not measure journal diameter before ordering will receive standard-grade bearings that either bind or allow excessive oil film clearance. The big-end bore on this connecting rod must also be measured for out-of-round and taper, because a prior rebuild that honed the bore beyond specification will not hold a bearing shell correctly even with new fasteners. Engine serial variants across the C3.4 and 3044C platforms introduce differences in rod bolt thread pitch and cap alignment method, making blind cross-referencing a frequent source of fitment failure [NEED_CITE: crankshaft journal measurement and bearing grade selection for aftermarket rebuilds].
High-strength forged steel construction provides the fatigue resistance needed to survive repeated combustion loading without crack initiation, which is why magnetic particle inspection is specified — surface and near-surface discontinuities that visual examination misses become failure origins under cyclic stress. The center-to-center length tolerance of ±0.05 mm ensures that piston deck height remains consistent across all cylinders, preventing compression ratio variation that would otherwise cause uneven combustion temperatures. Big-end bearing surface finish at Ra ≤0.4 μm is essential because rougher finishes abrade bearing shells during the initial run-in period, accelerating wear before the oil film stabilizes. Hardness in the HRC 32–36 range balances tensile strength with sufficient toughness to resist impact loading at top dead center, where the rod experiences a reversal from compression to tension in a fraction of a crankshaft revolution.
Replacing a failed connecting rod without investigating the lubrication fault or over-fueling condition that caused the original failure simply resets the clock on the same failure mode. Oil pump degradation, clogged galleries, and injector drip all produce bearing starvation or thermal overload that a new rod and bearing set cannot survive. Workshops that skip oil pressure testing and gallery flushing before reassembly regularly see the replacement rod fail within a few hundred hours. The cost is not the part — it is the second teardown, the second gasket set, the second round of machine downtime [NEED_CITE: lubrication system failure modes leading to connecting rod bearing damage].
Production lines and sourced supply operate under one account with identical quality control and warranty terms, so the connecting rod and its matched bearing set arrive from a single source with consistent documentation. Eight product categories mean a complete overhaul list — rods, pistons, bearings, gaskets, fasteners, oil pump, and seal kits — ships as one consolidated consignment rather than staggered deliveries from separate vendors. Minimum order from one piece supports single-cylinder repairs without forcing a full engine set purchase. Guangzhou warehouse stock on fast-failure items keeps common rebuild components available for immediate dispatch. Part identification extends beyond the number itself: machine model, nameplate photograph, or worn component image all feed into cross-reference verification that covers superseded numbers and alternate variants. Technical support confirms bearing grade, bolt specification, and weight class before the order is released.
Provide the engine serial number, any known crankshaft regrind history, and the bearing grade used in the previous overhaul. If the engine plate is unreadable, a photograph of the old connecting rod and the adjacent piston assembly allows identification. This information enables confirmation of the correct rod variant, matched bearing set, and compatible fastener specification before the order is processed.
Q: What con rod bearing grade pairs with this connecting rod for my engine build? A: The correct bearing grade depends on whether the crankshaft journals were reground during a prior overhaul. Standard-size shells fit unmachined journals, while undersize grades (0.25 mm, 0.50 mm) correspond to ground journals. Provide the engine serial number and any rebuild records so we can confirm the matching bearing set for this connecting rod.
Q: How do I confirm whether my crankshaft journals have been ground and to what undersize? A: Physical measurement of journal diameter with a micrometer is the only reliable method. Rebuild paperwork or stamped markings on the crankshaft counterweight may indicate the grind size. If records are unavailable, measure before ordering bearing shells to avoid clearance mismatch.
Q: Should I replace all connecting rods as a set or only the failed one? A: Replacing only the failed rod is acceptable if the remaining rods pass dimensional inspection and weight matching checks. However, if the engine has high hours or an unknown rebuild history, replacing the full set ensures consistent weight balance and bearing clearance across all cylinders.
Q: What lubrication system checks should be done before reassembly to prevent repeat failure? A: Verify oil pump output pressure, flush all block galleries, inspect the oil cooler for internal leakage, and confirm the pressure relief valve operates within specification. Connecting rod bearing failure frequently originates upstream in the lubrication circuit rather than in the rod itself.
Q: Does the overhaul gasket kit include the rod bolt seals and fasteners I need? A: Standard overhaul gasket kits typically cover head, sump, and crankcase seals but may not include torque-to-yield rod bolts or rod bolt seals. Confirm the kit contents against your specific engine build variant, and add fastener sets if required to complete the rebuild.
<p>Overhaul kit contents verified item-by-item against your specific V1505 build before dispatch</p>
View Details<p>Stop losing uptime to camshaft-related misfires, rough idling, or failed emissions tests — this <strong>exhaust camshaft</strong> delivers OEM-matched timing accuracy and lift profile right out of the box, restoring smooth power delivery and valve train harmony in your 2.0L Gamma engine.</p> <ul> <li>Direct-fit replacement for Hyundai Elantra (2016–2020), Kona (2018–2021), Veloster (2019–2021), and Kia Forte/Seltos/Soul (2019–2024) — no machining or adjustments needed</li> <li>Features hardened nitrided lobes and precision-ground journals — a critical spec that prevents premature wear on Gamma-series hydraulic lash adjusters</li> <li>Built to match original base circle diameter and lobe separation angle — ensures correct phasing with the intake cam and avoids ECU correction errors</li> <li>Ships from our Guangzhou warehouse with full traceability and 6-month warranty — no guesswork, no delays, no counterfeit risk</li> </ul>
View Details<p><strong>10200A 10202 10369A Timing Tool Kit for 3.6L Engines</strong> — aftermarket set including tension loosening wedges, phaser holder, and alignment tool for camshaft and timing chain service procedures.</p> <ul> <li>Supports precise valve timing during top-end overhaul on compatible VW, Chrysler, Dodge, and Jeep 3.6L applications</li> <li>Matches phaser, gasket, and seal kit replacements typically performed together in a matched valvetrain rebuild</li> <li>Suits high-hour fleet vans, mining support trucks, and agricultural equipment running 3.6L powerplants</li> </ul> <p>Overhaul kit contents verified item-by-item against engine serial before dispatch.</p>
View Details<p><strong>Push Rod 733817M1 Replacement for Massey Ferguson Powertrain</strong> — Forged SAE 1045 steel, quench-and-temper heat treated, phosphate coated. Fits Perkins-based diesel engines across Massey Ferguson, Oliver, and White tractors and combines (engine s/n 4.212, 4.248, 6.354, 1006.60, T4.236 variants). Part of the valve train system; replacement should include matched lifters, rocker arms, and valves for uniform wear across the set. Engine serial confirmation prevents fitment errors from variant differences.</p> <ul> <li>Overhaul kit contents verified item-by-item before dispatch</li> </ul>
View DetailsSend us your inquiry and our technical team will verify the part and provide a competitive quote within 24 hours. MOQ starts from 1 piece.
Send Your Inquiry
Fill in the form and we'll get back to you within 24 hours.