Engine Serial Variants Verified — each cylinder head matched to specific V1505 build configurations to prevent valve train mismatch during overhaul.
Technical Specifications
| Parameter |
Value |
| Part Number |
16060-03044, 1G092-03044, 1G871-03040, 1G679-03040, KEACK-1G092, KU-KEACK-1G871 |
| Product Type |
Cylinder Head |
| Cross-Reference |
16060-03044, 1G092-03044, 1G871-03040, 1G679-03040, KEACK-1G092, KU-KEACK-1G871 (reference only) |
| Machine Fitment |
B3030HSD, B3030HSDC, B3030HSDCC, B3000HSDC, B3000HSDCC, B3200HSD, B3200HSDWO, B3300SUHSD, B7800HSD, B7820HSD, B2910HSD, F3680, F3690-AU, KX71-3, KX71H, KX91-2, KX91-2S |
| Assembly State |
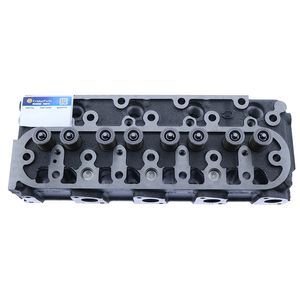
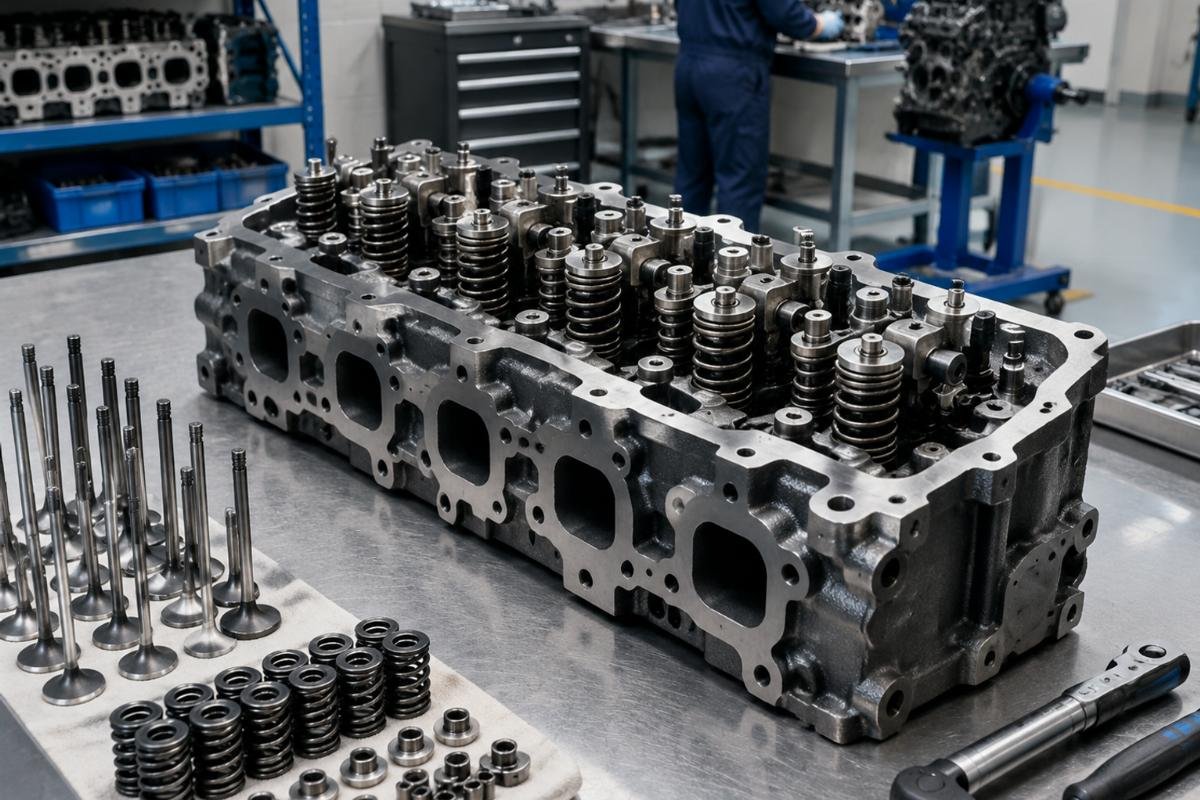
Complete assembly with intake/exhaust valves, valve springs, retainers, and valve guides installed |
| Casting Material |
Ductile iron (ASTM A536 Grade 65-45-12) |
| Valve Material |
Stainless steel (AISI 422) with hardened tips and nitrided stems |
| Valve Seat Hardness |
55–60 HRC |
| Deck Surface Flatness |
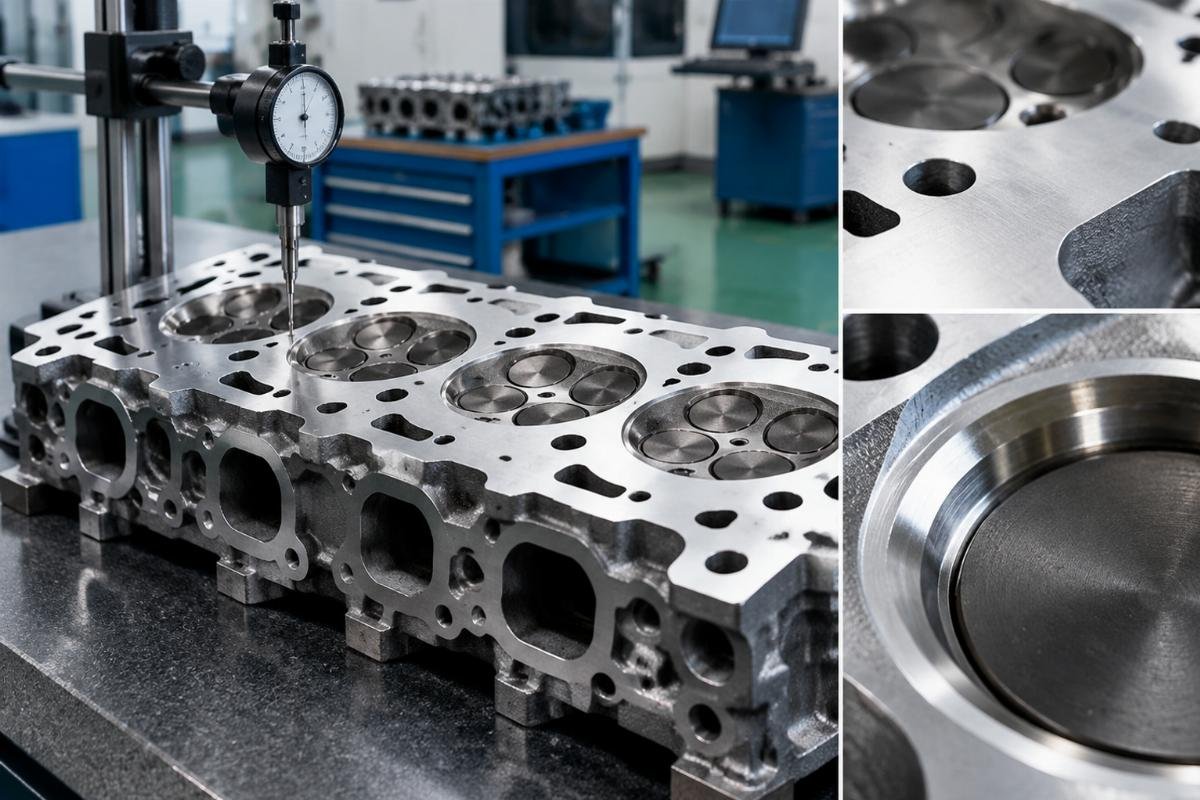
≤0.03 mm TIR |
| Valve Guide Material |
Bronze-sintered |
| Valve Guide Tolerance |
±0.005 mm |
| Stem-to-Guide Clearance |
0.03–0.05 mm |
| Engine Compatibility |
Kubota V1505, V1505-E3B, V1505-T, V1505-T-E2B, V1505-T-E3B, V1505-E2B-JICASE-2, V1505-E3B-KEA-1, V1505-E4B-VMR-1, and 40+ documented variants |
| Warranty |
3–12 months against manufacturing defects |
| MOQ |
1 piece |
| Standards |
ISO 9001, ISO 8535-2, SAE J2430 |
Application Suitability
| Engine System |
Related Components |
| Complete V1505 Valve Train |
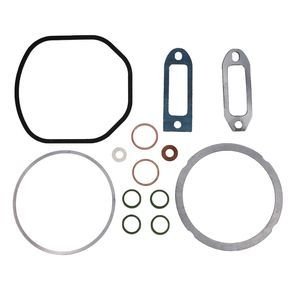
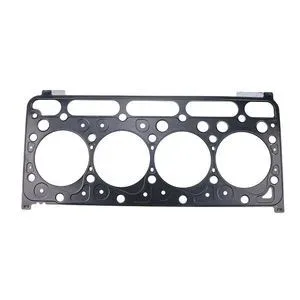
Head gasket, valve cover gasket, intake and exhaust manifold gaskets, head bolts |
| Post-Overheat Rebuild |
Coolant thermostat, water pump, radiator cap, coolant hoses |
| Valve Seat Recession Repair |
Intake and exhaust valves, valve stem seals, injector sleeves |
| High-Hour Fleet Overhaul |
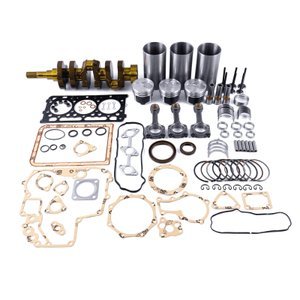
Piston rings, main and rod bearings, oil pump, full gasket kit |
Why the Same Cylinder Head Part Number Ships in Multiple Variants
Internal valve train dimensions shift across V1505 production runs, making engine serial confirmation essential before dispatch.
When rebuilding compact tractor and mini-excavator engines, shops frequently encounter a situation where the casting looks identical, but the installed valve springs or guide lengths differ between early and late production serial ranges. [NEED_CITE: Kubota V1505 engine serial variant documentation for aftermarket parts identification]. Swapping a head assembled for a V1505-T-E2B onto a V1505-E3B block without verifying the internal build sheet leads to incorrect valve lash, poor combustion sealing, or piston-to-valve contact. This Kubota V1505 Cylinder Head for Engine Overhaul & Rebuild requires the specific engine serial to ensure the valve train geometry matches the block's deck height and camshaft profile. Rebuild facilities that skip this verification step often face teardowns within the first hundred hours of operation.
System-Level Matching for V1505 Combustion Sealing
The cylinder head does not function in isolation; it forms the upper boundary of the combustion chamber and houses the entire valve actuation interface. When a Kubota V1505 Cylinder Head for Engine Overhaul & Rebuild arrives as a complete assembly, the valve springs, retainers, and guides are already matched to the casting's port geometry and seat angles. This eliminates the risk of reusing fatigued springs from a failed head, which is a common root cause of early valve float and subsequent seat damage in high-cycle compact equipment engines.
Addressing the Root Cause Behind Repeat Head Failures
Many cylinder head replacements fail prematurely because the underlying thermal or mechanical stress was never resolved. [NEED_CITE: diesel engine cylinder head thermal fatigue failure modes in compact equipment]. If the previous head suffered from valve seat recession, simply installing a new casting without inspecting the cooling system passages, verifying injector spray patterns, and checking for block deck warpage invites a repeat failure. Our approach requires confirming whether the engine block has undergone previous machining, as resurfacing the block deck changes the compression geometry and may require a different head gasket thickness to maintain proper valve clearance.
Material Specifications and Thermal Load Management
The ductile iron casting, specified to ASTM A536 Grade 65-45-12, provides the thermal fatigue resistance necessary for the rapid load cycling typical of mini-excavator and compact tractor duty cycles. These machines frequently transition from idle to high-load digging or PTO operation, creating steep thermal gradients across the head. The induction-hardened valve seats at 55–60 HRC directly address the recession failure mode that follows sustained high-load operation, which is the root cause behind many repeat head gasket complaints. The deck surface is machined to ≤0.03 mm TIR, ensuring uniform head gasket compression and eliminating coolant leakage paths that are often misdiagnosed as gasket quality issues. The bronze-sintered valve guides, held to ±0.005 mm tolerance, maintain the 0.03–0.05 mm stem-to-guide clearance required for proper oil control and valve stem cooling.
The Hidden Cost of Ignoring Engine Build History
Sending a standard-assembly head to an engine that has already been bored oversize or deck-resurfaced in a previous rebuild creates compression ratio mismatches and valve timing errors. [NEED_CITE: engine rebuild machining tolerance stack-up effects on compression geometry]. The shop then faces a second teardown to source thicker head gaskets or different pushrod lengths, adding days of downtime and freight costs. This is particularly common in fleet operations where machines have passed through multiple ownership cycles and rebuild records are incomplete.
Sourcing Strategy for Rebuild Facilities
We maintain production on selected cylinder head lines and source the remainder from qualified ISO-certified manufacturing partners, with both carrying identical quality control and warranty terms. Our technical team verifies cross-reference numbers against superseded and alternate listings, which is critical given that Kubota V1505 part numbers have been updated across multiple machine generations. We supply from one piece minimum, allowing rebuild shops to order a single sample head for fitment verification on a specific engine serial before committing to bulk inventory for their compact equipment fleet. The Guangzhou warehouse holds stock on common V1505 configurations for fast dispatch, and we provide part identification from engine serial numbers, photographs of the existing nameplate, or the machine model alone when the engine tag is missing.
Documentation & Verification
- Commercial invoice and packing list detailing specific V1505 engine serial variant matched.
- Part compatibility and cross-reference sheet marking OEM numbers as reference only.
- Quality inspection record covering combustion chamber leak test and deck flatness certification.
- Warranty terms specifying coverage against manufacturing defects for 3 to 12 months.
- Packing photographs showing valve train protection and port covers before crating.
- HS code and customs documentation support for international engine parts shipment.
Installation & Rebuild Sequence
- Verify block deck flatness and previous machining history before positioning the new cylinder head.
- Clean all head bolt holes in the block to ensure accurate torque readings during installation.
- Install new head bolts and follow the manufacturer's multi-stage torque and angle sequence.
- Set valve lash to specification after the head has reached operating temperature and cooled once.
- Prime the lubrication system before initial startup to prevent dry running of the valve train.
Requesting Fitment Confirmation
To ensure the correct Kubota V1505 Cylinder Head for Engine Overhaul & Rebuild is dispatched, provide the full engine serial number from the block nameplate, any visible casting numbers on the existing head, and details of any previous block machining such as deck resurfacing or bore oversizing. This allows our technical team to cross-reference the specific valve train configuration required for your engine variant.
Frequently Asked Questions
Q: What components are included in the complete cylinder head assembly, and what else should I order for a full overhaul?
A: The assembly includes the ductile iron casting with intake and exhaust valves, valve springs, retainers, and bronze-sintered guides installed. For a complete V1505 overhaul, you should also order the head gasket, valve cover gasket, intake and exhaust manifold gaskets, and new head bolts to ensure proper clamping force and sealing across the entire combustion system.
Q: How do I confirm which V1505 engine variant my machine has when the same model uses different serial configurations?
A: Locate the engine serial number stamped on the block nameplate, typically near the injection pump or oil filter housing. Provide this serial number along with the machine model, such as B3030 or KX71-3, so we can verify the specific valve train geometry and cross-reference the correct cylinder head assembly for your exact production run.
Q: If my engine block has been resurfaced in a previous rebuild, does that affect which cylinder head or gasket I need?
A: Yes, block resurfacing reduces the deck height and alters compression geometry. You must measure the amount of material removed and provide this data so we can determine if a thicker head gasket is required to maintain proper valve-to-piston clearance and combustion chamber volume for your V1505 engine.
Q: Can I get a sample unit for fitment verification before committing to a bulk order for my rebuild shop?
A: Yes, we supply from a one-piece minimum order quantity specifically to allow rebuild shops to test fitment on their specific engine serial variants. Once you confirm the valve train geometry and port alignment match your V1505 configuration, you can proceed with bulk inventory orders for your fleet maintenance program.