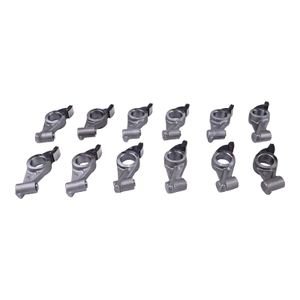
Engine Serial Variant Confirmed — We cross-check cylinder head casting numbers against the five OEM supersession paths before dispatching this valve train set, preventing geometry mismatches that surface only after the head is torqued down.
Technical Specifications
| Parameter |
Value |
| Part Number |
13257-40F06 |
| Product Type |
Rocker Arm |
| Cross-Reference |
13257-40F06, 1325740F06, 13257-40F07, 13257-40F17, 13257-40F16 (reference only) |
| Machine Fitment |
Nissan Pickup (Hardbody) 2.4L KA24E SOHC 12V (1989–1997), Nissan Stanza 2.4L (1989–1992), Nissan 240SX 2.4L (1989–1991), Nissan Axxess 2.4L (1990–1995) |
| Material |
High-carbon steel (SAE 1045 equivalent) |
| Assembly State |
Complete set |
| Oil Feed Holes |
Drilled to OEM diameter and depth |
| Condition |
New Aftermarket |
| Warranty |
6 months against manufacturing defects |
| MOQ |
1 piece |
| Standards |
ISO 9001, ISO 8533, JIS-D0202 |
Application Suitability
| Engine System |
Related Components |
| Valve train assembly |
Camshaft lobes, valve stems, valve springs, stem seals |
| Cylinder head rebuild |
Head gasket set, valve guides, valve seat inserts |
| Lubrication to pivot |
Oil gallery passages, cam bearing feed holes, rocker shaft oil ports |
| Emission and combustion |
Valve timing alignment, compression sealing, ignition synchronization |
Why a Rocker Arm Set KA24E Engine Rebuild Replacement Demands System-Level Verification
The failed rocker arm rarely failed alone — it is a symptom of oil starvation, cam lobe scoring, or altered head geometry from a previous resurfacing.
Rebuild shops regularly encounter KA24E heads where the deck was machined flat during a prior overhaul, shifting the rocker arm contact geometry relative to the valve stem tip. When a standard-grade rocker arm set is then installed without accounting for that material removal, the contact patch migrates toward the edge of the valve stem, accelerating wear on both surfaces. I have handled cases where separate procurement of valve train components led to dimension mismatches between parts sourced from different suppliers, requiring a second teardown [NEED_CITE: valve train geometry verification after cylinder head resurfacing]. The cost of that second head removal far exceeds the price of verifying the complete system before assembly begins.

Valve Train System Context and Adjacent Wear
A rocker arm set KA24E engine rebuild replacement does not operate in isolation. Each arm pivots against the camshaft lobe profile on one end and contacts the valve stem tip on the other, transmitting lift force while enduring sliding friction at the fulcrum. When one rocker shows significant pivot wear, the corresponding cam lobe has likely sustained matching damage. Replacing the rocker without inspecting or renewing the camshaft invites the new arm to ride on a worn lobe profile, generating abnormal contact stress and premature failure. Engine rebuild shops quoting a complete valve train refresh should evaluate cam bearings, valve spring pressure, and stem seal condition simultaneously to avoid a return visit within months.
Prior Rebuild History and Dimension Grade Alignment
Production of the KA24E spans nearly a decade across multiple vehicle platforms, and cylinder heads in the field have often been opened before. A previous rebuild may have fitted oversize valve guides, replaced valves with different stem lengths, or resurfaced the head deck beyond factory tolerance. Each of these modifications alters the installed geometry that the rocker arm must accommodate [NEED_CITE: effects of cylinder head resurfacing on valve train geometry]. Before ordering, confirm the head casting number and measure valve stem protrusion to determine whether the standard rocker arm geometry remains correct. Requesting a quality inspection record that documents lift ratio validation for the supplied batch provides an additional safeguard against geometry-related failures.
Material and Hardness Specifications Interpreted for Service Conditions
The high-carbon steel construction (SAE 1045 equivalent) provides the bulk strength necessary to transmit cam lift forces across thousands of operating cycles without deformation. Drilled oil feed holes ensure that pressurized lubricant reaches the pivot point continuously, which is the primary wear surface during operation. When these passages are obstructed or undersized, metal-to-metal contact at the fulcrum accelerates dramatically. The complete set supply means every cylinder receives arms with matched material properties and dimensional tolerances, preventing cylinder-to-cylinder imbalance that manifests as uneven idle or localized valve noise [NEED_CITE: valve train lubrication requirements for SOHC engines].
The Hidden Cost of Mismatched Valve Train Components
When rebuild shops source rocker arms, valve springs, and stem seals from separate suppliers without verifying dimensional compatibility, the resulting mismatch often remains invisible until the engine is running under load. A rocker arm with a slightly different pivot ratio than the adjacent cylinder's spring pressure expects will alter valve opening duration on that cylinder, causing combustion imbalance. I recall a case involving separate procurement of engine components where dimensional incompatibility between parts was discovered only after the engine was assembled and running rough. Correcting that situation required full disassembly, component replacement, and a second round of machining [NEED_CITE: valve train mismatch consequences in overhead cam engines]. The labor hours consumed by that corrective cycle dwarf the effort of ordering a verified matched set from the start.
Why Rebuild Shops Source This Component Through Our System
Our production and sourcing operations cover eight component categories under a single account and warranty, meaning a complete KA24E overhaul — from rocker arms to piston rings to gasket sets — ships as one consignment with matched lead times. Every part number is verified against engine serial variants, including the five cross-reference designations applicable to this rocker arm set, so supersession paths across production years are resolved before dispatch. The minimum order quantity of one piece accommodates emergency single-cylinder repairs without forcing a full set purchase. Guangzhou warehouse stock on common valve train items enables fast dispatch when a head rebuild cannot wait for extended production cycles. Our technical team confirms fitment against head casting numbers and prior rebuild history, not just against catalog listings. Sample supply before bulk commitment lets shops verify contact pattern and pivot fitment on their specific head.
Documentation & Verification
- Commercial invoice and packing list itemizing every rocker arm by position number
- Cross-reference sheet mapping 13257-40F06 through 13257-40F17 supersession (reference only)
- Dimensional inspection record covering lift ratio and pivot bore tolerance
- Six-month warranty terms covering manufacturing defects from dispatch date
- Packing photographs showing set completeness before crate closure
- HS code classification and customs documentation for international engine parts shipments
Installation & Rebuild Sequence
- Verify head deck thickness before installing to confirm rocker geometry remains within specification
- Clean all oil feed passages in the head and rocker shaft before assembly to ensure pivot lubrication
- Install the complete rocker arm set as matched units, never mixing old and new arms across cylinders
- Check valve stem contact pattern on each arm after initial lash adjustment to confirm centered loading
- Prime the oil system before first start to prevent dry pivot contact during initial cranking cycles
- Re-torque rocker shaft fasteners after the first heat cycle per manufacturer sequence
Requesting a Fitment-Verified Quote
Provide your KA24E engine serial number and cylinder head casting number so we can confirm which of the five cross-reference designations applies to your specific build. If the head has been resurfaced or fitted with oversize valves during a prior rebuild, share those machining records for dimensional compatibility verification. Photographs of the existing rocker arm set and adjacent valve train components help us identify any variant differences that catalog data alone may not resolve.
Frequently Asked Questions
Q: What other valve train components should be replaced alongside the rocker arm set during a KA24E head rebuild?
A: Valve stem seals, valve springs, and camshaft bearings should be evaluated and typically renewed during the same teardown. The camshaft lobes that contact each rocker arm should be inspected for scoring or profile wear. If any lobe shows significant material loss, replacing the rocker arms without addressing the cam will cause the new arms to wear prematurely. Complete valve train kits consolidating these components avoid a second disassembly.
Q: How do I determine if my KA24E head has been resurfaced before ordering rockers?
A: Measure the head thickness at multiple points using a straight edge and compare against factory specifications. Visible machining marks on the deck surface or the absence of casting flash on the combustion chamber edges indicate prior resurfacing. Excessive material removal alters rocker arm geometry relative to valve stem tips. Our technical team can review your measurements and head casting number to confirm compatibility before dispatch.
Q: Are all five OEM reference numbers interchangeable for the same engine?
A: The numbers 13257-40F06, 13257-40F07, 13257-40F16, 13257-40F17, and 1325740F06 represent supersession paths across production revisions of the KA24E platform. They are not universally interchangeable across all engine serial ranges. Confirming your specific engine serial and head casting number allows us to identify which designation applies to your build and verify correct rocker arm geometry for your application.
Q: What oil system issues commonly cause premature rocker arm wear on the KA24E?
A: Blocked oil galleries in the cylinder head, worn cam bearings reducing oil pressure to the upper valvetrain, and degraded oil pump output all starve the rocker pivot of lubrication. Before installing new arms, flush all oil passages and verify oil pressure at the head gallery. Installing new rockers without resolving the starvation cause results in the same failure pattern repeating within a short operating period.
Q: How do I confirm my specific engine serial to ensure correct fitment?
A: Locate the engine serial number stamped on the cylinder block, typically near the transmission bell housing mating surface. Cross-referencing this serial against the vehicle build date and head casting number establishes which production revision your engine represents. Photographs of the existing rocker arms and the head casting markings help our team verify the correct variant from the five applicable reference numbers before confirming your order.