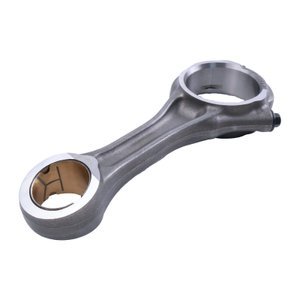
System-Matched Supply — Every connecting rod ships with verified cross-reference data and grade confirmation tied to your D24NAP engine serial number.
Technical Specifications
| Parameter |
Value |
| Product Type |
Connecting Rod |
| Part Number |
7032360 |
| Cross-Reference |
7032360 (reference only) |
| Machine Fitment |
Doosan D24NAP Engine |
| Material |
Forged 42CrMo alloy steel |
| Yield Strength |
≥950 MPa |
| Ultimate Tensile Strength |
≥1100 MPa |
| Big-End Bore Tolerance |
±0.005 mm |
| Surface Treatment |
Shot-peened |
| Inspection Method |
Magnetic particle inspection |
| Certification |
ISO 9001 |
| Standards |
ISO 6892-1, SAE J429 Grade 8.2 |
| Condition |
New Aftermarket |
| Warranty |
6 months against manufacturing defects |
| MOQ |
1 piece |
Application Suitability
| Engine System |
Related Components |
| Crank-rod mechanism |
Piston, piston pin, con rod bearing, main bearing |
| D24NAP full overhaul |
Overhaul kit including gaskets, seals, and fasteners |
| Single-cylinder repair |
Replacement requires crankshaft grinding history verification |
| Rebuild shop inventory |
Matched-grade connecting rod and bearing shell sets |
When the Overhaul Kit Arrives but the Grades Do Not Align
A connecting rod 7032360 engine rebuild fails not from the rod itself but from mismatched size grades across the crank-rod group.
I once stood over a dismantled D24NAP in a high-altitude mine site, watching a technician hold a standard-grade connecting rod against a crankshaft that had clearly been reground. The overhaul kit had arrived on schedule, yet the entire job stalled because the bearing shells needed a 0.25 oversize while the rods were supplied at STD [NEED_CITE: engine rebuild grade matching practices for heavy diesel engines]. When one component in the crank-rod group has been reworked, every mating part must follow. The downtime from a single grade error often exceeds the time lost waiting for correct parts to arrive.

Where This Rod Sits Inside the D24NAP Crank-Rod System
The connecting rod 7032360 links piston reciprocation to crankshaft rotation, transferring combustion loads through the big-end bearing into the main journal. In the D24NAP four-cylinder configuration, each rod must maintain matched weight class and bore grade with its adjacent pistons and bearing shells. Swapping a single rod without verifying the grade of the remaining set introduces imbalance that accelerates wear across the entire rotating assembly.
Rebuild History Dictates What You Actually Need
Before ordering, the crankshaft grinding record determines whether the big-end bore accepts STD, 0.25, or 0.50 oversize bearing shells, and the rod must accommodate that same grade [NEED_CITE: crankshaft regrind grade selection for medium-speed diesel engines]. Different engine serial numbers within the D24NAP range may carry variant crankpin diameters from the factory. Providing the engine serial number allows verification of the exact crankpin specification and ensures the connecting rod and bearing set form a dimensionally coherent group.
What Forged 42CrMo and Shot Peening Mean in Practice
Forged 42CrMo alloy steel delivers yield strength above 950 MPa, giving the rod beam resistance to the compressive and shear loads generated during each combustion cycle. The big-end bore tolerance of ±0.005 mm controls oil film thickness between the rod journal and the bearing shell — too tight starves the bearing, too loose causes impact loading. Shot peening introduces compressive residual stress on the surface, which retards fatigue crack initiation under the thousands of load reversals a mining engine endures daily. Magnetic particle inspection catches subsurface forging defects that visual checks miss entirely [NEED_CITE: magnetic particle inspection standards for forged engine components].
The Cost of Skipping Grade Verification
When a rod arrives at the wrong oversize grade, the technician either forces assembly with incorrect bearing clearance or halts the rebuild entirely. Forced assembly leads to early bearing wipe, often within the first hundred hours of operation. A halted rebuild means the block sits open on the bench, exposed to contamination while waiting for replacement parts. Either outcome multiplies the original repair cost through wasted labor and secondary component damage.
Why Source This Rod Through XUNPO
Selected connecting rod lines are produced in our own Guangzhou facility, while sourced supply from ISO-certified partners carries identical QC and warranty terms. Eight product categories under one account mean the overhaul kit, gasket set, and bearing shells consolidate into a single shipment. Minimum order starts at one piece, so an emergency single-rod replacement ships without padding a larger order. Part identification works from a part number, machine model, or a photograph of the nameplate — useful when paint and grime obscure the stamping. Cross-reference verification covers superseded numbers, and a sample can ship for fitment confirmation before bulk commitment.
Documentation & Verification
- Commercial invoice and packing list matched to your D24NAP overhaul order
- Cross-reference sheet confirming 7032360 (reference only) compatibility with your engine serial
- Dimensional inspection report covering big-end bore and center distance
- Magnetic particle inspection record for each connecting rod
- Warranty terms document covering six months against manufacturing defects
- Packing photographs showing rod protection and crate condition before dispatch
Installation & Rebuild Sequence
- Verify crankshaft journal grade before fitting the connecting rod bearing shells
- Confirm rod bolt stretch or torque-to-angle per D24NAP service manual specification
- Check big-end bore roundness after torquing to catch any distortion from handling
- Match piston-to-rod assembly weight across all four cylinders within tolerance
- Perform initial run-in at reduced load to seat new bearing shells against the journal
Requesting a Matched Quote
Provide your D24NAP engine serial number and any known crankshaft regrind history. If the nameplate is unreadable, send a photograph of the existing rod stamping or the engine block casting number. This allows the technical team to confirm the correct size grade and assemble a matched set of rods, bearings, and related overhaul components before quoting.
Frequently Asked Questions
Q: What else should an overhaul kit include alongside the connecting rods?
A: A complete D24NAP overhaul kit should contain pistons, piston pins and circlips, con rod and main bearing shells at the correct oversize grade, full gasket set, piston rings, and rod bolts. Each item must match the same size grade dictated by the crankshaft regrind history. Missing circlips or wrong-grade bearings are common kit gaps that halt reassembly.
Q: The crankshaft has been reground — what grade of rod and bearing do I order?
A: Once the crankshaft journals have been reground, the connecting rod big-end bore and bearing shells must match that oversize grade, typically STD, 0.25, or 0.50. Measure the crankpin diameter or provide the machinist's grind record. Supplying mismatched grades forces either destructive assembly or a full rebuild stoppage.
Q: Do all D24NAP engines share the same connecting rod part number?
A: The D24NAP range may carry crankpin diameter variants across different engine serial numbers, even though the base part number remains the same. Providing your specific engine serial allows verification of the exact dimensional variant. This prevents ordering a rod that physically fits but operates outside the specified bearing clearance.
Q: What typically causes connecting rod failure beyond normal wear?
A: Rod failures often trace back to lubrication starvation from oil pump degradation or blocked galleries rather than simple overload. Before installing a replacement rod, inspect the oil feed passages in the crankshaft and block. Addressing the root cause prevents the new connecting rod 7032360 engine rebuild from repeating the same failure cycle within months.