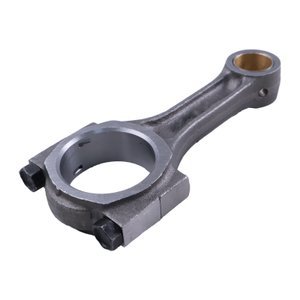
Matched Set Verified — Crankshaft journal grade, piston pin bore, and bolt spec cross-checked against your exact 3TNA72 suffix variant before dispatch.
Technical Specifications
| Parameter |
Value |
| Part Number |
3TNA72 |
| Product Type |
Connecting Rod |
| Cross-Reference |
3TNA72, 3TNA72UJ, 3TNA72L, 3TNA72E, 3TNA72E-G2, 3TNA72E-GB2, 3TNA72E-HP, 3TNA72E-NC, 3TNA72E-S, 3TNA72E-UAS, 3TNA72E-UNS, 3TNA72E-YL, 3TNA72L-UDW, 3TNA72L-UDW2, 3TNA72L-UKS, 3TNA72L-UMCD, 3TNA72L-UMS, 3TNA72L-UTBZ, 3TNA72L-UWD (reference only) |
| Machine Fitment |
YB121, YB151, FF165, FF155, F145, 430, 455, 755, 670, F925 |
| Material |
Forged 42CrMo alloy steel |
| Heat Treatment |
HRC 32–36 |
| Big-End & Small-End Bore Surface Roughness |
Ra ≤0.8 μm |
| Journal Diameter |
42.98–43.00 mm |
| Center-to-Center Length |
135.0 ±0.05 mm |
| Crankshaft Journal Tolerance |
±0.005 mm |
| Bearing Bore Roundness |
≤0.012 mm |
| Straightness |
≤0.03 mm/m |
| Tensile Strength |
850 MPa |
| Surface Treatment |
Phosphate coating |
| Salt-Spray Resistance |
72-hour |
| Condition |
New Aftermarket |
| Warranty |
3–12 months against manufacturing defects |
| MOQ |
1 piece |
| Standards |
ISO 9001, SAE J429 Grade 8.8 |
Application Suitability
| Engine System |
Related Components |
| Crankshaft-piston assembly |
Con rod bearings matched to crankshaft journal grade |
| Cylinder block rebuild |
Piston pin bushings and circlips for the specific 3TNA72 variant |
| Lubrication system diagnosis |
Oil pump and pickup screen to rule out starvation as root cause |
| Gasket sealing interface |
Head gasket and crankcase seals included in matched overhaul kit |
| Fastener integrity |
Connecting rod bolts meeting SAE J429 Grade 8.8 torque specification |
Why the Crankshaft History Decides Which Connecting Rod Goes In
A connecting rod shipped without knowing the engine's rebuild history is a guarantee of repeat failure.
Over the years, I have seen too many teardowns where the old crankshaft was ground to a 0.25 undersize during a previous overhaul, and the next shop installed standard-size bearing shells on it. The oil pressure dropped within hours. The same pattern repeats: a workshop orders a replacement connecting rod based on the engine model alone, ignoring that the crankshaft journal was machined down in a prior rebuild [NEED_CITE: engine rebuild practice and undersize bearing selection]. When the new rod arrives with standard bearings, the clearances are wrong, and the engine is torn down again. This is not a parts defect — it is an information gap. The Yanmar 3TNA72 Connecting Rod for Engine Overhaul must be paired with the correct bearing grade, and that grade depends entirely on what happened inside the block before.

System Adjacency Demands a Matched Approach
A connecting rod never fails in isolation. It sits inside a system where the piston pin bore, the crankshaft journal surface, the bearing shell thickness, and the lubrication oil flow all interact at every revolution. When sourcing a Yanmar 3TNA72 Connecting Rod for Engine Overhaul, the adjacent components — con rod bearings, piston pin bushings, crankshaft main bearings, and the head gasket — must arrive as a verified matched set. Mismatched tolerances between the rod bore and the bearing shell create localized hot spots that accelerate wear far beyond normal progression.
Serial Variants and Oversize Grades Change the Equation
The 3TNA72 engine family includes suffix variants such as 3TNA72E, 3TNA72L, 3TNA72UJ, and others, each potentially differing in piston pin diameter, rod bolt thread specification, or balance weight configuration [NEED_CITE: engine serial variant differences in compact diesel platforms]. A standard connecting rod ordered by base model alone may not align with a variant-specific bolt torque or pin bore. Beyond variants, prior regrinding of the crankshaft journals introduces undersize grades — STD, 0.25, 0.50 — and each demands a specific bearing shell thickness to maintain the designed oil film. Installing standard shells on a reground journal causes immediate oil pressure loss and bearing spin.
Reading the Specifications Against Real Rebuild Conditions
The forged 42CrMo alloy steel provides tensile strength rated at 850 MPa, which resists the cyclic bending loads typical in compact excavators and agricultural tractors under repeated shock loading. The HRC 32–36 heat treatment balances core toughness with surface hardness, preventing the rod from stretching under peak combustion pressure while maintaining enough ductility to absorb impact without brittle fracture. The center-to-center length held to 135.0 ±0.05 mm ensures that piston-to-valve clearance remains within design limits after assembly — even a small deviation here changes compression ratio and valve timing geometry. Big-end and small-end bore surface roughness at Ra ≤0.8 μm allows the bearing shells to seat evenly, avoiding localized contact pressure that leads to premature bearing fatigue. Bearing bore roundness at ≤0.012 mm keeps the oil film uniform around the full journal circumference, which is critical for hydrodynamic lubrication at idle and low-RPM operation [NEED_CITE: hydrodynamic bearing film requirements in small-bore diesel engines].
The Cost of Skipping the Root-Cause Check
Replacing a failed connecting rod without diagnosing why it failed is setting up the next failure. The most common root causes — oil starvation from a clogged pickup screen, over-torque on rod bolts during a previous assembly, or contamination in the lubrication system — will destroy the new rod just as quickly [NEED_CITE: common root causes of connecting rod failure in diesel engines]. A workshop that swaps the rod and reassembles without pulling the oil pan and inspecting the pump is likely to see a second teardown within the first hundred operating hours. The cost is not the rod itself — it is the labor, the additional gasket set, the bearing kit, and the machine downtime all over again.
Why Rebuild Shops Source This From Our Guangzhou Facility
Our production lines and qualified sourcing partners operate under the same warranty and QC protocol, so whether your order is one rod or a full overhaul kit, the dimensional checks are identical. We verify crankshaft journal condition, piston pin bore, and bolt spec against your exact engine serial suffix before confirming the match. Guangzhou warehouse stock covers common 3TNA72 variants for prompt dispatch, while the technical team cross-references superseded numbers when your nameplate is worn or painted over. A single-piece sample ships first if you need fitment confirmation before committing to a bulk rebuild kit order.
Documentation & Verification
- Commercial invoice listing each 3TNA72 variant and matched bearing grade
- Cross-reference sheet covering all suffix variants (reference only)
- Dimensional inspection record for bore roundness and straightness
- Warranty terms specifying coverage against manufacturing defects
- Packing photographs showing rod protection and labeling before crate closure
- HS code and customs classification support for international engine parts shipment
Installation & Rebuild Sequence
- Verify crankshaft journal diameter with a micrometer before selecting bearing shells for the new connecting rod
- Clean all oil galleries and the pickup screen to eliminate starvation as a repeat failure cause
- Torque rod bolts to the SAE J429 Grade 8.8 specification in the staged sequence
- Check piston-to-valve clearance after installing the rod-and-piston assembly into the bore
- Run initial break-in at reduced load to allow bearing shells to seat against the journal surface
Requesting an Accurate Match
Provide the full engine serial number including the suffix variant, any known crankshaft regrind history, and the target bearing grade if already measured. If the nameplate is unreadable, a photograph of the existing connecting rod alongside the piston pin allows our team to confirm the variant and ship the correct matched components.
Frequently Asked Questions
Q: What other components should be replaced alongside a new connecting rod during an overhaul?
A: Con rod bearings, piston pin bushings, circlips, and rod bolts should all be replaced as a matched set. The head gasket and crankcase seals are also recommended since the block is already open. Sourcing these together ensures dimensional compatibility across the entire crankshaft-piston system and avoids a second teardown for a missed component.
Q: How can I tell if my crankshaft has been reground and what bearing grade I need?
A: Measure the crankshaft journal diameter with a micrometer and compare it to the standard specification. If the reading is below the standard range, the journal was reground to an undersize grade such as 0.25 or 0.50. The replacement bearing shells must match this undersize to maintain correct oil film clearance.
Q: Are connecting rods identical across all 3TNA72 suffix variants?
A: No. Suffix variants within the 3TNA72 family can differ in rod bolt thread specification, piston pin bore diameter, and balance weight configuration. Ordering by base model alone risks a mismatch. Confirm the full serial number including suffix to ensure the correct variant ships.
Q: What typically causes a connecting rod to fail, and how do I prevent it from happening again?
A: Common causes include oil starvation from a clogged pickup screen or failing oil pump, over-torque on rod bolts during prior assembly, and contamination in the lubrication system. Inspecting the entire lubrication circuit and replacing the pickup screen during reassembly addresses the root cause rather than just the symptom.
Q: How do I confirm my exact engine serial number if the nameplate is worn or painted over?
A: A clear photograph of the existing connecting rod, the piston pin, and any legible casting marks on the block allows our technical team to narrow down the variant. Cross-referencing these physical features against known serial configurations identifies the correct suffix and corresponding component specifications.