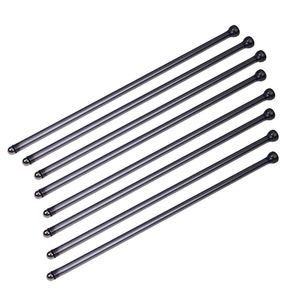
Matched Sets Shipped — Push rods matched to C2.2/C1.1 valve train specs, bundled with lifters and seals in one overhaul dispatch to eliminate mid-rebuild parts mismatches.
Technical Specifications
| Parameter |
Value |
| Part Number |
154-1248 |
| Cross-Reference |
1541248, CA1541248 (reference only) |
| Product Type |
Push Rod |
| Material |
High-carbon forged steel |
| Engine Compatibility |
CAT 3034, 3024C, C2.2, 3024, C1.1 |
| Machine Fitment |
Skid Steer Loaders: 216, 216B, 226, 226B, 228, 232, 232B, 232D, 242, 242B; Compact Track Loaders: 239D, 249D; Multi Terrain Loaders: 247B, 257B; Excavator: 304.5; Compactor: CB-334E, CB34, CC34 |
| Condition |
New Aftermarket |
| Packaging |
8 pcs per set, individual protective sleeve |
| Quality Standard |
ISO 9001 |
| Warranty |
6-month warranty against manufacturing defects |
Application Suitability
| Engine System |
Related Components |
| Valve Train Rebuild (C2.2/C1.1) |
Hydraulic lifters, rocker arms, valve stem seals |
| Cylinder Head Service (3034/3024C) |
Head gasket set, camshaft bearings, push rod guide plates |
| Bottom End Overhaul |
Piston ring sets, connecting rod bearings, crankshaft thrust washers |
| Scheduled Top-End Refresh |
Tappets, valve springs, injector sleeves |
Why Valve Train Failures Return After a Rebuild
Replacing the failed part without diagnosing the system that destroyed it guarantees repeat downtime.
Workshops often quote a C2.2 push rod engine rebuild based on the bent components found during teardown, missing the worn cam lobe or scored lifter bore that caused the push rods to fail in the first place. The machine runs for a few hundred hours before the new rods bend again [NEED_CITE: common root causes of repeated valve train failure in small displacement diesel engines]. In a skid steer loader operating at high RPM on a demolition site, a single cylinder losing valve timing shuts down the entire machine until the head comes off again.
System Context for the Valve Train Assembly
These push rods transfer motion from the camshaft lifters to the rocker arms in the CAT 3034, 3024C, C2.2, 3024, and C1.1 engine families. They operate in a system where hydraulic lifters, cam lobes, and rocker arms must wear at a matched rate; when one component is replaced with a different material grade or dimensional tolerance, the adjacent parts absorb the mismatch. A Push Rod engine rebuild only succeeds when the entire valve train is inspected as a single system rather than a collection of individual line items.
Matching Dimensional Grade to Engine Rebuild History
Engines in the C2.2 and C1.1 families have often been rebuilt once or twice before arriving in a workshop, and previous rebuilds may have used oversized bearings or variant-grade components. Ordering standard push rods for an engine that has had its lifter bores honed or its camshaft reground can result in incorrect valve lash and premature contact fatigue. Confirming the engine serial number and reviewing the teardown measurements against the factory specification sheet prevents ordering parts that are dimensionally close but functionally incompatible [NEED_CITE: engine serial variant identification procedures for multi-generation diesel platforms].
Material Traceability and Heat Treatment Consistency
The high-carbon forged steel construction of these push rods provides the compressive strength required for the high-frequency loading in compact equipment engines. Consistent heat treatment across all eight rods in a matched set ensures uniform thermal expansion, which maintains valve lash settings as the engine reaches operating temperature. In generator set applications where the C2.2 runs at constant RPM for extended periods, even minor variation in rod length or material hardness between cylinders causes uneven valve timing and localized exhaust temperature spikes that damage downstream components.

The Hidden Cost of Unmatched Rebuild Kits
A workshop that sources push rods, lifters, and gaskets from three separate suppliers to chase individual line-item savings often discovers during assembly that the lifter diameter does not match the push rod socket profile. The engine block is already apart, the head is on the bench, and the machine sits dead until the correct components arrive. This mid-rebuild stall turns a scheduled three-day overhaul into a two-week delay, with the customer's compact track loader missing its next contract [NEED_CITE: cost impact of split-shipment delays during heavy equipment overhauls]. The secondary damage from forcing mismatched parts together—scored lifter bores, bent valves, damaged cam bearings—can exceed the cost of the entire valve train kit.
Why Sourcing Through This Account Differs
Production on selected engine part lines is completed in-house, while sourced components from qualified manufacturing partners carry the same quality control protocol and warranty terms, so a complete overhaul kit ships under one accountability. Eight product categories mean the push rods, gasket sets, filters, and seal kits for a full C2.2 rebuild consolidate into a single dispatch. Orders start from a single piece for emergency repairs, and the Guangzhou warehouse holds stock of fast-failure items for immediate release. Part identification works from the worn number, the machine model plate, or a photograph of the nameplate when paint and debris obscure the original stamping. Cross-reference verification covers superseded numbers and alternate references across engine generations, and sample supply is available for fitment confirmation before a workshop commits to a fleet-wide overhaul program.
Documentation & Verification
- Commercial invoice listing each push rod set with engine serial cross-reference
- Compatibility sheet confirming C2.2 and C1.1 variant applicability
- Dimensional inspection record covering rod length and tip profile
- Warranty certificate detailing the manufacturing defect coverage period
- Packing photographs showing sleeve protection before box closure
- HS code classification for customs clearance documentation support
Installation & Rebuild Sequence
- Verify push rod length matches teardown measurement before installation
- Inspect each lifter bore for scoring before seating new hydraulic tappets
- Install push rods in original cylinder order if reusing adjacent components
- Set valve lash to engine serial specification after initial cranking
- Run first start at idle for break-in before applying load
Provide Engine Details for Rebuild Confirmation
Submit the engine model, serial number, and any available rebuild history to receive a matched component list that accounts for variant differences within the C2.2 and C1.1 families. Photographs of the existing nameplate and the torn-down valve train components allow the technical team to verify grade and dimensional requirements before dispatch.
Frequently Asked Questions
Q: What other valve train components require inspection during push rod replacement?
A: Camshaft lobes, hydraulic lifter bores, and rocker arm pivot points must be measured against factory specifications during teardown. Worn cam profiles or scored lifter bores that are not addressed during the same rebuild will destroy the new push rods within the first service interval, as the root cause of the original failure remains active in the system.
Q: How do engine serial variants affect push rod compatibility within the C2.2 family?
A: Engine serial numbers identify specific production runs that may carry different valve train configurations, including variations in push rod length and socket profile. Confirming the serial number ensures the supplied components match the exact build specification, preventing the installation of dimensionally similar but functionally incompatible parts from adjacent production variants.
Q: What inspection records accompany the supplied push rod set?
A: Each batch ships with a dimensional verification record covering rod length and tip geometry, along with material certification confirming the high-carbon forged steel specification. These documents support warranty claims and provide the rebuild shop with traceable quality evidence for the customer's maintenance file.
Q: How can a workshop confirm whether an engine has been previously rebuilt?
A: Teardown measurements of cylinder bore diameter, crankshaft journal size, and lifter bore clearance compared against the original factory specification sheet reveal oversized components from prior rebuilds. This inspection determines whether standard or variant-grade push rods and associated components are required for the current overhaul to maintain correct system tolerances.