Block & Internal Parts
Rebuild Kit Connecting Rod Compatible with Kubota V3307 Engine
<p>Overhaul kit contents verified against your engine variant before dispatch</p>
View Details
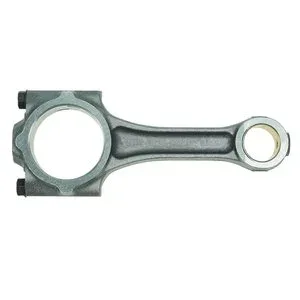
<p><strong>Connecting Rod 1L5Z-6200-A</strong> — replacement for Ford 2.3L L4 gasoline engines (2006–2011), forged 4340 alloy steel, shot-peened finish with precision oil groove for wrist pin lubrication.</p> <ul> <li>System-matched supply with con rod bearings, piston assemblies, and overhaul gasket kits ensures correct pairing across the bottom end</li> <li>Bearing clearance grade (STD/0.25/0.50) verified against crankshaft machining history before dispatch</li> </ul> <p>Overhaul kit contents cross-checked item by item against your engine build variant.</p>
MOQ
1 Piece
Lead Time
2-5 Business Days
Shipping
120+ Countries
Warranty
3-12 Months
Compatible Brands
System-Matched Supply — Rod sets ship with verified bearing grade charts to align with your crankshaft's machining history.
| Parameter | Value |
|---|---|
| Part Number | 1L5Z-6200-A |
| Product Type | Connecting Rod |
| Cross-Reference | 1L5Z-6200-A (reference only), 1L5Z6200A (reference only) |
| Machine Fitment | Ford Fusion (2006–2009), Ford Ranger (2009–2011), Lincoln MKZ (2007–2009), Lincoln Zephyr (2006), Mercury Milan (2006–2009) |
| Engine Application | Ford 2.3L L4 gasoline engine (2006–2011) |
| Condition | New Aftermarket |
| Material | Forged 4340 alloy steel |
| Big-End Bore Tolerance | ±0.01 mm |
| Pin Bore Tolerance | ±0.005 mm |
| Surface Finish | Ra ≤0.8 μm |
| Oil Groove | Precision-machined for wrist pin lubrication |
| Standards | ISO 9001, FMVSS 106, ISO 6892-1, SAE J2430, ASTM E112 |
| Engine System | Related Components |
|---|---|
| Bottom-End Rotating Assembly | Con rod bearings, main bearings, crankshaft |
| Piston & Cylinder Group | Piston assemblies, wrist pins, cylinder honing |
| Lubrication Circuit | Oil pump, oil galleries, wrist pin oil feed |
| Sealing & Gasket System | Overhaul gasket kit, rear main seal, pan gasket |
Addressing the root cause of the original failure prevents the new assembly from suffering the same fate.
When a Connecting Rod engine rebuild happens in isolation, the underlying fault — often oil starvation or a spun bearing — remains in the block. I have seen rebuilt engines fail within weeks because the adjacent lubrication passages were not flushed or the crankshaft journal was not measured for taper. A replacement 1L5Z-6200-A unit must be treated as part of a system-level correction rather than a simple swap [NEED_CITE: engine rebuild root cause analysis procedures for L4 platforms].
This connecting rod transfers combustion loads from the piston to the crankshaft journal, operating under continuous tensile and compressive stress cycles. In the Ford 2.3L L4, it sits within a tightly packaged bottom end where bearing clearances directly influence oil film stability. A Connecting Rod engine rebuild must account for the entire rotating assembly to maintain balance and load distribution across all four cylinders.
Crankshafts on these engines are frequently reground after a bearing failure, shifting journal diameters into oversize territory. Ordering a standard-grade rod without confirming the crankshaft's current machining state leads to incorrect bearing crush and rapid wear. We verify the required bearing clearance grade — whether STD, 0.25, or 0.50 oversize — before dispatching matched sets, so the assembly fits the block as it stands today rather than as it left the factory [NEED_CITE: crankshaft regrind tolerance standards for aftermarket engine rebuilding].
The forged 4340 alloy steel construction provides the fatigue strength necessary for sustained high-RPM operation in the 2.3L platform. Big-end bore tolerance held at ±0.01 mm ensures consistent bearing crush across all cylinders, which is critical for maintaining hydrodynamic oil film thickness. The pin bore tolerance of ±0.005 mm controls wrist pin float, preventing scuffing against the piston bosses. Shot-peening introduces compressive residual stress on the surface, delaying crack initiation at the rod beam's stress concentration points.
Fitting a new rod without measuring crankshaft journal taper or checking oil gallery blockage invites repeat failure under load. Shops that skip the teardown inspection frequently see the replacement Connecting Rod engine rebuild fail at the same cylinder within a short operating window. The cost of a second teardown, new gaskets, and additional machining far outweighs the time spent on initial system verification [NEED_CITE: typical cost of secondary engine failure after incomplete rebuild].
Our production and sourcing lines operate under one warranty, covering both the rod and its matched bearing set from a single account. Eight product categories allow a complete overhaul kit — rod, bearings, pistons, gaskets — to ship as one consignment rather than staggered deliveries. Minimum order starts at one piece for emergency single-cylinder repairs. Our technical team confirms bearing grade and engine serial variant compatibility before the order ships, and we provide cross-reference verification covering superseded numbers so the correct part reaches your bench.
Send us the engine serial number, crankshaft machining history, and the specific cylinder positions requiring replacement. We will return a system-matched quote covering the connecting rod, bearing grade, piston assemblies, and overhaul gasket set as one consolidated package.
Q: What other components should be replaced alongside this connecting rod during a 2.3L L4 rebuild? A: A complete bottom-end overhaul typically includes matched con rod bearings, main bearings, piston ring sets, and a full gasket kit. Replacing only the rod without addressing the bearings and seals risks contamination from worn adjacent parts entering the new assembly, shortening its service life.
Q: How do I determine the correct bearing grade if the crankshaft was previously machined? A: Measure each crankshaft journal with a micrometer and compare readings against the bearing manufacturer's clearance chart. Previous regrinds may have moved journals into 0.25 or 0.50 oversize territory, requiring corresponding undersize bearing shells to maintain correct oil film thickness.
Q: Are there internal differences across 2.3L engine serial variants that affect rod fitment? A: Yes, production changes across the 2006–2011 model years introduced variations in wrist pin diameter and oil groove geometry. Providing the engine serial number or casting code allows us to verify the correct rod variant before shipment, avoiding fitment issues on the bench.
Q: Can you supply a matched overhaul kit including this rod, bearings, pistons, and gaskets? A: We consolidate rod assemblies, bearing sets, piston groups, and gasket kits into one shipment under a single warranty. Each kit is built to match the specific engine serial variant and crankshaft machining state you report, reducing the risk of mismatched components arriving from separate suppliers.
Q: How do I determine whether the original rod failure was caused by an oil system fault? A: Inspect the failed bearing shell for embedded debris, discoloration patterns, and wipe marks that indicate oil starvation. Check the oil pump pickup screen for blockage and verify oil gallery passages are clear, as these upstream faults will destroy a new connecting rod just as quickly as the original.
<p>Overhaul kit contents verified against your engine variant before dispatch</p>
View Details<p>Stop downtime caused by worn or failing rocker levers on your Cummins X15 and ISX engines — this <strong>rocker lever 4059353</strong> delivers OEM-equivalent strength, precision geometry, and consistent valve actuation so your engine runs smoothly under heavy load.</p> <ul> <li>Direct-fit replacement for Cummins ISX and X15 engines — no machining or adjustments needed</li> <li>Manufactured to original Cummins tolerance specs: ±0.002 mm rocker tip radius and hardened 42CrMo alloy steel for fatigue resistance</li> <li>Backed by our 6-month warranty and pre-shipment performance verification — no guesswork, no counterfeit risk</li> <li>In-stock in Guangzhou and ships in 2–5 working days, even for single-piece orders</li> </ul>
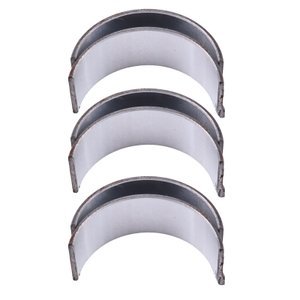
View Details<p>Stop engine knock and extend your Kubota D722 or EA300’s service life with precision-matched STD connecting rod bearings that deliver OEM-equivalent fit, load capacity, and oil clearance — right out of the box. No more guessing at tolerances or risking downtime from premature bearing failure.</p> <ul> <li><strong>Direct replacement for 15531-22310</strong> — includes 3 full pairs (6 shells) with correct eccentricity and crush fit for proper journal seating</li> <li>Fits not just D722 & EA300, but 10+ Kubota engine families including V1100, Z482, and E75-NB3-HG-2 — one part number covers your entire fleet’s small diesel line</li> <li>Each set is pre-gapped to <strong>0.02–0.04 mm radial clearance</strong> — verified with optical bore gauges, not just stamped specs</li> <li>Ships same-day from Guangzhou warehouse: no 3-week waits or price markups just to get back in operation</li> </ul>
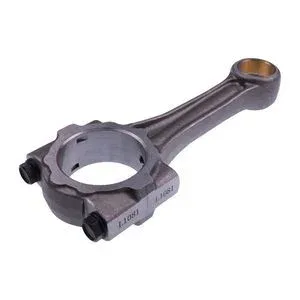
View Details<p><strong>Connecting Rod for Kubota V2403-M, V2403, V2403M engines, New Aftermarket</strong> — replacement for cranktrain system rebuilds where bearing clearance grade and piston-rod match determine reliability.</p> <ul> <li>Belongs to the block and internal system; must be matched with correctly graded <strong>con rod bearings</strong>, piston assemblies, and a variant-specific overhaul gasket set to align with the engine's prior rebuild history</li> <li>Oil starvation is a common root cause — lubrication passages and pump output should be verified before reassembly</li> <li>Confirm exact engine serial to avoid V2403 vs V2403-M internal differences</li> </ul> <p>Overhaul kit contents verified item-by-item before dispatch to match your engine build.</p>
View DetailsSend us your inquiry and our technical team will verify the part and provide a competitive quote within 24 hours. MOQ starts from 1 piece.
Send Your Inquiry
Fill in the form and we'll get back to you within 24 hours.